Picture an automotive bracket. If its job is to carry vibration, hold a threaded boss, and bolt into a machined housing, CNC machining from solid aluminum is usually the safer choice. The material is predictable, threads can be machined cleanly, and critical dimensions can be controlled closely.
Now picture that same bracket rebuilt with topology optimization. Three separate components become one, with internal channels and a significantly reduced weight. That is where 3D printing can win, because you cannot mill a lattice or internal passage that a cutting tool cannot physically reach.
The question in 3D printing vs CNC machining is not which process is universally better. It is which process fits the part.
When Should You 3D Print vs CNC Machine a Part?
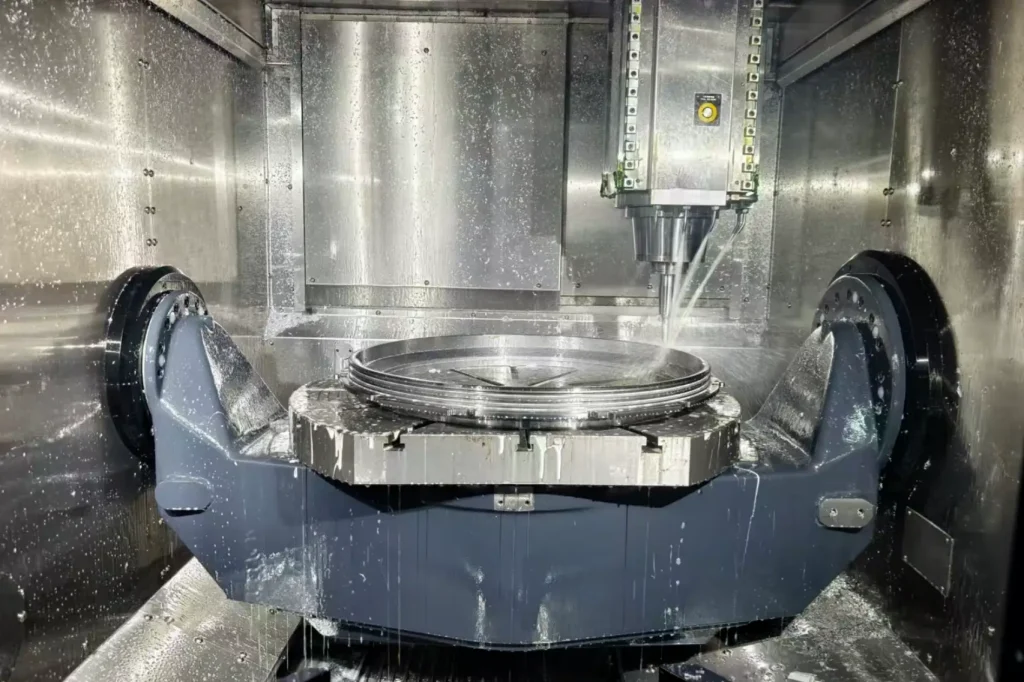
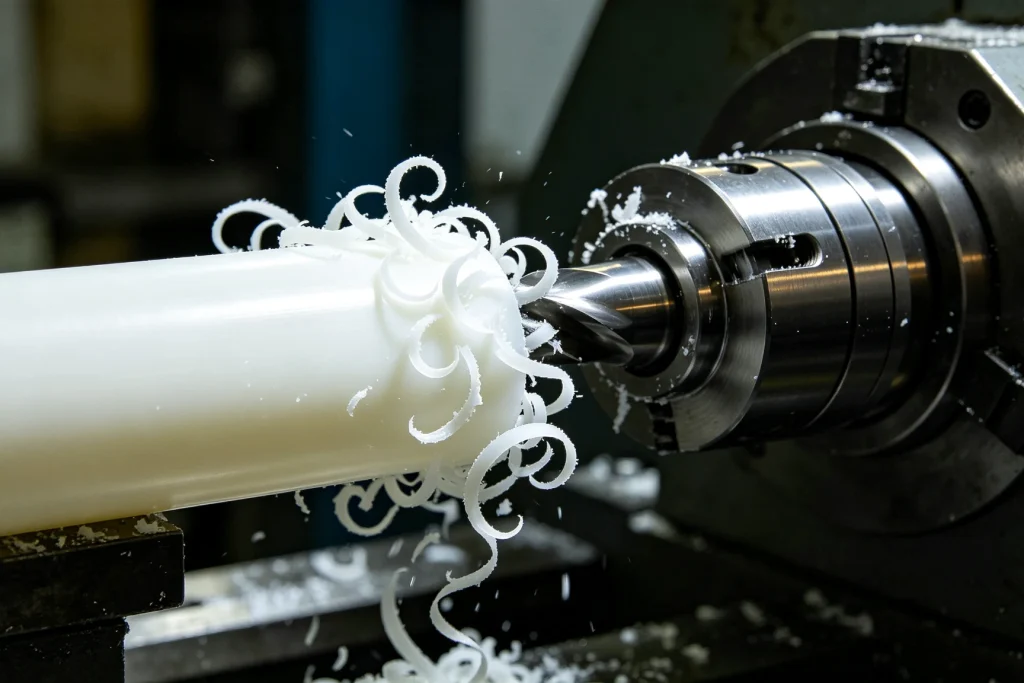
CNC machining starts with a solid block, bar, or other stock and removes material until the required geometry is produced. It offers a broad selection of engineering materials and is particularly well suited to parts requiring tight tolerances, controlled surface finishes, and repeatable production.
3D printing, or additive manufacturing, builds a part layer by layer. It can produce internal channels, lattices, organic shapes, and other geometries that may be difficult or impossible to reach with conventional cutting tools.
When a part combines both requirements, the two processes can also be used together: 3D printing creates the complex near-net shape, while CNC machining finishes the critical interfaces.
A Decision Shortcut: Match the Process to Your Part
CNC Machining Is Usually a Better Starting Point When:
| Part requirement | Why |
| Tight tolerances on functional features | CNC provides tighter and more predictable dimensional control |
| A specific metal grade is required | CNC supports a broad range of established engineering materials |
| The geometry is accessible to cutting tools | Conventional holes, pockets, faces, and other features are generally straightforward to machine |
| Many identical production parts are needed | Setup and programming costs can be distributed across the production run |
| Surface finish is critical | CNC can achieve controlled finishes such as Ra 3.2 μm and finer finishes on suitable features |
3D Printing Is Usually a Better Starting Point When:
| Part requirement | Why |
| Complex internal geometry is required | Internal channels and enclosed features can be built without conventional tool access |
| Lattice or topology-optimized structures are needed | Additive manufacturing enables geometries that are difficult or impossible to machine |
| Several components can be consolidated | Multiple components can potentially be redesigned as a single part |
| Low-volume complex parts are needed | No dedicated cutting tooling may be required, depending on the process |
| Tool access is the main manufacturing limitation | Geometry is built layer by layer rather than constrained by cutting-tool access |
Neither process is automatically better. The right choice depends on the complete combination of geometry, material, quantity, tolerance, surface finish, and application requirements. If your part is still a prototype and other routes like vacuum casting or sheet metal are also on the table, our rapid prototyping services guide compares those options too.

Geometry: Where 3D Printing and CNC Machining Differ Most
Geometry is often the first technical question an engineer should ask.
CNC machining works especially well when cutting tools can reach the required features. Open pockets, flat faces, accessible holes, bosses, and conventional prismatic shapes are generally straightforward to machine.
3D printing becomes more attractive when the design contains:
- Internal channels or enclosed passages
- Lattice structures
- Organic or freeform surfaces
- Topology-optimized structures
- Features that would require multiple components to manufacture conventionally
- Geometry that would require unusually complex tooling or multiple setups
This does not mean that every complex shape should be printed. Support structures, build orientation, post-processing, material requirements, and inspection can all affect the final result.
For many engineering parts, the best solution is to redesign the geometry around the manufacturing process rather than simply choosing one process for the existing CAD model.
Tolerances and Surface Finish: What Each Process Actually Holds
| Process | Typical dimensional tolerance* | Typical surface roughness* | Common post-processing / finishes |
| CNC machining | ±0.05–0.10 mm; down to ±0.005 mm on selected features | Ra 3.2 μm typical; Ra 0.8 μm achievable | Anodizing, passivation, electropolishing, plating, bead blasting, polishing |
| Metal 3D printing (DMLS/SLM) | Typically ±0.1–0.2 mm | Typically Ra 10–25 μm | Machining, bead blasting, polishing, material-specific surface treatments |
| SLS | Typically ±0.25 mm | Typically Ra 10–25 μm | Bead blasting, tumbling, dyeing, vapor smoothing |
| MJF | Typically ±0.30 mm | Typically Ra 10–25 μm | Bead blasting, tumbling, dyeing, vapor smoothing |
*Actual results vary with material, geometry, machine, orientation, and inspection requirements. Surface finishes are material- and process-dependent.
CNC machining can achieve tight tolerances and controlled surface finishes on appropriately designed features. At FastPreci, tolerances around ±0.005 mm are achievable on selected tightly controlled metal features, while surface roughness around Ra 0.8 μm can be achieved on suitable surfaces.
3D-printed parts generally have rougher as-built surfaces and may require additional post-processing for functional or cosmetic requirements. Machining is commonly used on critical features such as precision bores, threads, bearing seats, and sealing surfaces, while bead blasting, polishing, tumbling, or material-specific surface treatments can improve appearance and surface quality.
The key is not simply asking whether a process can achieve a certain tolerance or finish, but which features actually need it. A hidden internal wall may allow more variation than a bearing bore or sealing surface.
3D Printing vs CNC Machining: Which Is Cheaper?
There is no universal quantity at which 3D printing becomes cheaper than CNC machining. Cost depends on geometry, material, part size, tolerances, machine time, setup requirements, post-processing, and production volume.
For one-off and low-volume parts, 3D printing can be attractive because it may reduce the need for dedicated fixtures and extensive machining setup, particularly when the geometry is complex. For simple parts, however, CNC machining can already be cost-effective at low quantities when the machining cycle is straightforward.
As volume increases, CNC often becomes more competitive because programming, setup, tooling, and other fixed costs can be distributed across more parts. Material economics also matter. Additive manufacturing can use material efficiently because it builds material where needed, but metal powders and engineering-grade polymers can have relatively high material costs. CNC machining typically starts from standard stock materials, which can be economical at scale, although more material may be removed during machining.
A practical way to compare the two is to request both routes using the same CAD model and quantity. The comparison should include:
- Manufacturing cost
- Setup, programming, and tooling
- Material cost
- Post-processing
- Inspection
- Lead time
3D Printing vs CNC Machining: Which Is Stronger?
Strength is not simply a question of whether a part was printed or machined. It depends on the material, manufacturing process, heat treatment, geometry, and loading conditions.
For metal additive manufacturing, build orientation can influence mechanical properties. For example, EOS Ti64 data shows different as-built yield strengths in the horizontal (XY) and vertical (Z) directions: approximately 1140 MPa and 1120 MPa respectively for the cited process and material condition.
NIST research also identifies build orientation and process parameters as important factors in the anisotropic behavior of additive-manufactured parts.
Strength data also varies by alloy — our metal 3D printing materials comparison covers eight SLM alloys with as-printed versus post-processed properties.
This does not mean that every 3D-printed metal part is weak. Industrial metal additive manufacturing can produce high-performance components with mechanical properties suitable for demanding applications. But the build direction, process parameters, heat treatment, surface condition, and inspection requirements need to be considered during design.
For load-bearing or fatigue-critical components, CNC machining from wrought material can provide a more predictable material baseline because the material does not have the same layer-by-layer build structure.
The right comparison is therefore not simply “printed vs machined.” It is the complete manufacturing process and the properties required by the application.
When 3D Printing and CNC Machining Work Together
What if a part has both highly complex geometry and tight precision requirements? In this case, 3D printing and CNC machining do not necessarily need to be competing options. They can be used together: additive manufacturing creates the complex geometry, while CNC machining finishes critical features that require tighter tolerances or better surface finishes.
This hybrid workflow is especially useful for:
- Internal channels combined with precision sealing surfaces
- Complex structures with precision mounting interfaces
- Near-net-shape metal components
- Topology-optimized parts with machined datum features
- Parts that need threads, bearing seats, or precision bores
The printer creates the geometry. CNC machining makes the critical interfaces work.

Case 1: 316L Cylinder With Internal Channels
A customer needed a 316L stainless steel cylinder with internal flow paths that would have been difficult or impossible to produce using conventional drilling.
We used SLM to build the internal geometry, then moved the part to five-axis CNC machining for the flange faces, bolt holes, and sealing surfaces. The printed structure created the internal passages, while machining brought the functional interfaces to the required dimensional and surface specifications.

Case 2: Ti6Al4V Ring With Conformal Airflow Channels
This Ti6Al4V ring contained internal airflow channels and thin-wall sections that could not be reached effectively with conventional cutting tools.
We printed the near-net shape, followed by stress relief and heat treatment. The part was then machined on a 5-axis CNC using low-force toolpaths and custom fixturing to protect the thin walls.
The result combined the geometric freedom of additive manufacturing with the precision of CNC machining.
Picking a Process by Industry
The same engineering principles apply across industries, but the priorities change.
- Automotive: A bracket that carries load goes CNC. A weight-optimized bracket goes print. Weight-critical programs favor printing for its shape freedom at low cost, and our 3D printed automotive parts guide lists the mistakes engineers make along the way.
- Medical: Metal additive manufacturing can produce porous or complex structures, while CNC remains important for precision instruments and functional interfaces.
- Semiconductor: CNC is widely used for precision fixtures and components requiring controlled materials and dimensional stability; additive manufacturing can support low-volume custom tooling.
- Robotics: Additive manufacturing can reduce weight in arm structures, while CNC is often preferred for high-load joints and precision interfaces.
- New Energy: Additive manufacturing can produce complex cooling channels, followed by CNC machining of sealing and mounting surfaces.
When a part sits between two process options, tolerance and load path are often two of the most important factors to evaluate.
Still Deciding between 3D Printing vs CNC Machining?
Send us your CAD file and requirements. We can evaluate the geometry, material, tolerance, quantity, and finishing requirements, then compare CNC machining, 3D printing, or a hybrid route where appropriate.
Instead of choosing a process first, we help determine which manufacturing route makes the most sense for the part.
FAQ
Is CNC machining more accurate than 3D printing?
For precision functional features, CNC machining generally provides tighter and more predictable dimensional control than most 3D printing processes. The actual tolerance depends on the material, geometry, machine, setup, and inspection method.
Is 3D printing cheaper than CNC machining?
Not always. 3D printing can be cost-effective for complex, low-volume parts because it may reduce setup and tooling requirements. CNC can become more economical for simple geometries and repeated production.
Is CNC machining stronger than 3D printing?
Not necessarily in every material or application. Industrial metal additive manufacturing can achieve high mechanical performance, but properties can vary with build orientation and process conditions. CNC machining from wrought material provides a more predictable material structure for many load-bearing applications.
When should I choose CNC machining over 3D printing?
Choose CNC when you need tight tolerances, specific material grades, controlled surface finish, or repeatable production of geometrically accessible parts.
Can a 3D-printed part be CNC machined afterward?
Yes. This is a common hybrid manufacturing approach. The part is printed close to its final shape, then CNC machining is used for threads, bores, bearing seats, sealing faces, mounting surfaces, or other precision features.
Will 3D printing replace CNC machining?
For most industrial applications, the more practical direction is not replacement but integration. Additive manufacturing is valuable where conventional machining has geometric limitations, while CNC remains essential for many precision production features. In many advanced components, the two processes work best together.