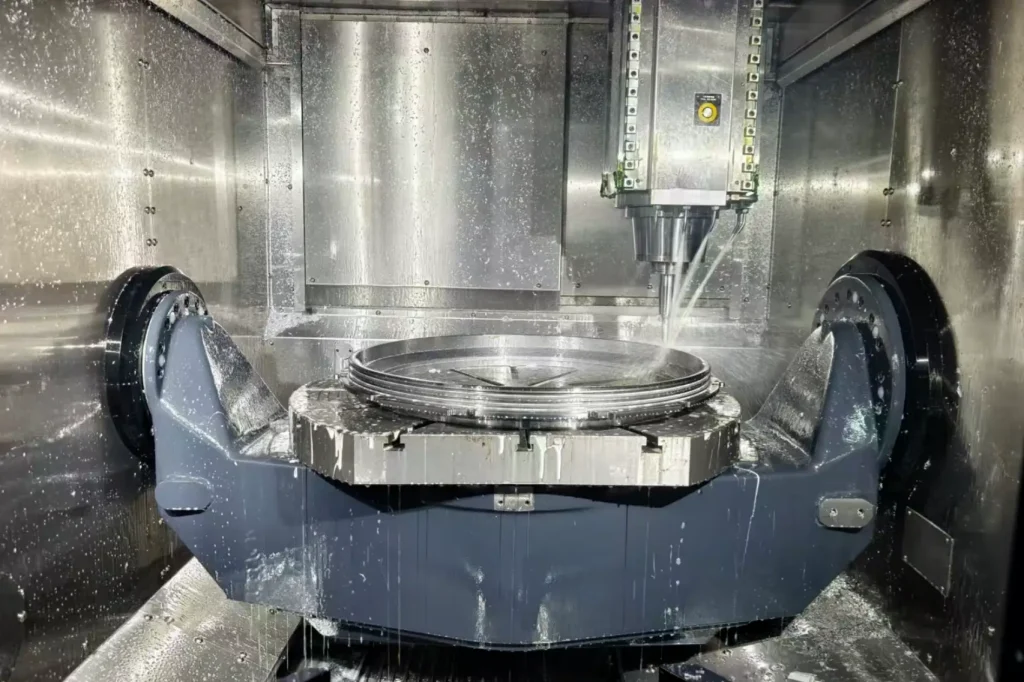
Large CNC machining follows different rules than the 3-axis work most engineers start with. Past about 1 m in any dimension, the problem stops being spindle power and becomes deflection, thermal growth, how you hold and load the part, and whether the shop can even move it.
Two things catch engineers out the first time they spec a large part. The shop flags a tolerance you didn’t think was tight. And the quote climbs because they need four setups and a crane just to move and hold the part. Both happen when a big part gets drawn and quoted like a small one with longer axes.
This guide follows the decisions in the order you face them: what “large” actually constrains, which machine fits the part, what tolerances survive at scale, what drives cost, when fabrication beats machining, and how to qualify a shop.

What “Large” Means in CNC Machining
“Large” covers a wide range of parts. A 12 m rail only 200 × 200 mm runs on a long gantry and is straightforward. A 6 m block, 1.5 m on a side and 20 tons, needs a floor-borer or large VTL plus a crane rated for the load. The word covers both, but they sit in different capability tiers, and three constraints decide which shops can take the job: length, cross-section, and weight.
Typical machine envelopes:
| Machine | X-travel | Typical load / range |
| Gantry / portal mill | 2,000–12,000+ mm | Table width 1,000–4,000 mm; several-ton class; floor-rail type removes the Y limit |
| Floor-type boring mill | 2,000–10,000 mm | Y 1,500–5,000 mm; bore spindle Ø110–200 mm; high table load |
| Vertical turning lathe (VTL) | Swing Ø 1,000–10,000 mm | Height 800–4,000 mm |
On a big part, weight limits your shop list as much as length. A 10-ton part needs a crane rated above the load plus fixture, and a floor rated for the point load. Many shops with a 12 m gantry still cap out at 5–8 tons because the foundation wasn’t built for it. Check crane capacity and floor-load rating before you shortlist, not just axis travel.
Before you ask for quotes, pin down three numbers: the longest side, the largest cross-section, and the raw weight. They set the shortlist of shops that can actually take the job.
If your part exceeds standard machining envelopes—or requires coordinated lifting, fixturing, multi-axis machining, and large-part inspection—work with a supplier that is equipped specifically for oversized components. Explore FastPreci’s large-part CNC machining services to review available capabilities and request a manufacturability assessment.
Gantry Mill, Boring Mill, or Vertical Lathe: Which One Fits Your Part
Match the machine to the part shape, not to its size.
| Part type | Best fit | Why |
| Long, flat prism / plate / beam | Gantry mill | Long X-travel, can extend on floor rails |
| Box or frame with bores on multiple faces | Floor-type boring mill | Bore spindle + rotary table put the hole pattern on target in one setup |
| Rotational part, flange, ring gear | Vertical lathe (VTL) | Turning accuracy and stable chucking |
| Features on more than one face plus internal cavities | 5-axis gantry / HMC | One setup removes the re-fixture error multi-face work introduces |
When no single machine covers the part, shops split the work. They rough on one machine and finish critical features on another, or index the part across stations. Indexing on a rotary table at fixed angles (4×90° or 6×60°) keeps every setup tied to the same datum. That is why a 4th or 5th axis pays off on prismatic parts with features on three or more faces.
Each handoff between setups reintroduces a locating error, and datum transfer becomes the main source of variation on a big part.
Tolerances on Large Parts: What Actually Holds
The first question on a large part is whether the tolerances will hold. They do, but only within a range that falls as the span grows.
| Feature length | Flatness / position typically held |
| 500 mm | 0.05–0.10 mm |
| 1,000 mm | 0.10–0.20 mm |
| 2,000 mm | 0.20–0.40 mm |
| 4,000 mm | 0.40–0.80 mm |
A competent shop with standard 3-axis equipment can hold these ranges. Treat them as achievable, not guaranteed, and ask each vendor for their own capability data.
Why does tolerance get worse with size? On a 4 m axis, the machine’s own geometric error (straightness and squareness) is no longer small. A single 0.02 mm leveling error at the fixture becomes 0.08 mm at the far corner. Add one re-clamp and the part can shift another 0.1–0.3 mm.
Thermal growth you must compensate
| Material | α (µm/m/°C) | 3,000 mm part, ΔT = 5°C |
| Steel | 11.7 | ≈ 0.18 mm growth |
| Cast iron | 10.8 | ≈ 0.16 mm |
| Aluminum | 23.0 | ≈ 0.35 mm |
In a shop without climate control, an 8–10°C daytime swing pushes a steel part past 0.3 mm, already wider than the tolerance. Control it by measuring at 20°C (ISO 1 / ASME Y14.5), using a laser tracker for in-process checks and letting the part settle to room temperature before final inspection.
Two shop practices decide whether a part holds tolerance. First, rough and finish in separate passes with 1–2 mm of stock left for finishing. Roughing dumps most of the heat and residual stress. Finishing removes the last clean layer.
Second, match the measuring tool to the span. A portable arm CMM covers up to ~3 m but loses accuracy at the far end. A laser tracker stays accurate across 10–30 m and is the standard for large weldments and aerospace frames.

Example: large sealed stainless chamber
One of our recent jobs was a sealed stainless chamber about 18 × 14 × 8 in. It carries O-ring grooves on both faces, internal water channels, and a thin wall between a channel and the main cavity. The two seal faces have to stay aligned. Reaching the second face means flipping the part, and that shift in datum is enough to break the seal or punch through the wall.
We machined it in a single 5-axis setup, with no flip: both seal faces, the water channels, and all bores cut in one pass. Tight tolerance went only where the part seals (O-ring grooves at ⌖0.001″ from Datum A, Ra0.8). The outline and the non-critical bores ran looser. Holding both faces on one datum is what kept the grooves aligned.

Example: large cylindrical aluminum heat-dissipator
FastPreci recently machined a cylindrical heat-dissipator in 6061 aluminum, Ø480 × 1,000 mm, with 18 longitudinal thread grooves around the circumference. The job needed CNC turning for the body, then 5-axis milling for the grooves.
The difficulty was the size and the grooves. At 1 m long the part is turned on a vertical lathe, then moved to a 5-axis mill for the grooves. Each machine change is a chance for the datum to shift, and if the grooves don’t line up with the turned body the part is scrap. The grooves are long and thin, so they deflect under the cutter and chatter if the pass is too heavy, something you don’t catch until inspection.
We turned the body on the VTL first to set a clean datum, then picked up that same turned diameter on the 5-axis mill for the grooves. Light passes and sharp tooling kept the grooves from deflecting, and we checked groove spacing at several points along the length rather than at one spot.
How to specify tolerance without inflating cost
- Use GD&T datums instead of a global ±0.05.
- Put tight tolerance only on mating surfaces; relax the rest to ±0.25–0.5. A bolt pattern that only locates a cover can run ±0.25 mm, while the seal groove it sits against needs ⌖0.05 mm. Specifying both at ±0.05 doubles inspection cost for zero function gain.
- Write explicit “non-critical” exemptions so the shop skips CMM points that add cost but no function.
What Drives Large CNC Machining Cost
Hourly rate is the least important number on the quote. A cheap machine that needs four setups and a full CMM sweep will out-cost a pricier 5-axis that does it in one. Read the cost through setups and inspections, not the hourly rate.
| Machine type | Rate tier | Note |
| Standard 3-axis VMC | $ | Most common, ample capacity |
| Large gantry (3-axis) | $ – $$ | Depends on travel and region |
| Floor-borer / large VTL | $$ – $$$ | Heavy equipment, few available spindles |
| 5-axis gantry / large 5-axis HMC | $$$ | High programming complexity + scarce capacity |
A large 5-axis machine typically costs well above a 3-axis gantry per hour, and the gap widens where capacity is scarce.
What pushes the quote up, in order of impact:
- Tight tolerance plus full CMM report. Inspection time can exceed cutting time.
- Multiple setups or re-fixturing. Each adds programming, datum verification, and risk.
- Material certs or heat-treat traceability. Documentation cost, mandatory in some industries.
- One-off or very low volume. Engineering and fixturing can’t be amortized.
- Expedite. Queue-jumping on a long-lead part.
- Third-party NDT (UT/PT/RT). Subcontract cost plus schedule dependency.
Engineering and fixturing commonly run 15–30% of the total job, and that share rises as volume drops. Precision inspection such as laser tracking is charged by the day and adds up fast on a large part.
To get a number you can trust, send the same print to at least three shops. Ask each for a line-item breakdown: material, machining hours by operation, engineering/fixturing, inspection, and freight. A quote that returns a single lump sum hides where the risk sits.
Watch for a shop that prices tight tolerance the same as loose. That usually means they missed the tight callouts, and the real cost shows up later as a re-quote or a part that fails inspection.
Machine the Solid, or Weld and Finish It
Which route fits depends on the part’s geometry.
- Near-net cast or forged blank exists: machine directly. Lowest risk.
- Part is mostly cavity or web structure: weld up, stress-relieve, finish-machine. Saves material and hours.
- Solid stock, overall mill: high material waste but no weld distortion or residual stress. Suits low-volume, high-rigidity parts.
Rule of thumb: when solid-stock removal exceeds ~60% and the part weighs several tons, fabrication’s material efficiency usually wins. Budget for post-weld stress relief (thermal or vibratory) and a finish-machining allowance.
Weld distortion is the catch. A fabricated frame can move 2–5 mm across its length as it cools. Leave 3–5 mm of finish stock on machined faces and plan a stress-relief cycle before the final pass. Skip it and the part shifts out of tolerance after it leaves the shop.
If the part has a sealed internal cavity (coolant or air channels), solid milling may be impossible because the tool can’t reach the inner walls. Fabrication plus finish machining is then the only practical route.
Packaging & Freight: What Happens After Machining
On a large part, one bad load can erase weeks of machining. Set the crating and freight plan before you approve the quote, not after the part is finished.
- Confirm crating is in the quote. A custom wooden crate with internal blocking and vibration-damping material takes shop time and material. Some shops include it, some bill it separately. Ask which, and what the crate is rated to carry.
- Freight mode follows weight and dimensions. Under roughly 150 kg / 330 lb ships less-than-truckload (LTL). Above that you are in full-truckload (FTL) or flatbed/oversize freight, where length drives cost as much as weight.
- Check the receiving end. Dock door height, forklift capacity, and crane access decide whether the crate can be unloaded at all. Measure the dock before the part ships, not on delivery day.
- Document before and after transit. Require photos of critical machined faces before crating. On receipt, inspect and record any damage immediately. Oversize-freight claims take longer to settle than standard parcels, so the record has to be in place at once.
For international sourcing, add customs paperwork and possible duties, and expect a longer transit where temperature swings can shift tight-tolerance features. Re-check critical datums after arrival.
How to Qualify a Large-Part Machining Shop
For a part this size, the specific shop matters more than the country it sits in. Ask for evidence, not promises.
| # | Request | What it verifies |
| 1 | Machine list: model, X/Y/Z travel, max load | They can physically hold the part |
| 2 | Recent photos of similar parts + a sample inspection report (CMM or laser tracker) | They’ve held this precision class |
| 3 | Material traceability process (heat/lot number, mill test report) | Required for critical parts |
| 4 | Quality certificates (ISO 9001 / AS9100 / IATF 16949) | Baseline process control |
| 5 | Two or three comparable customer references (can be anonymized) | Delivery record |
Red flags in a quote:
- Won’t publish machine travel or dodges max part size.
- Refuses to explain the fixturing and datum strategy.
- No inspection plan, or no clear method for how they’ll actually hold the tight tolerance.
- No clear method for tricky features, such as machining a thin wall without breaking through it.
A capable shop returns an inspection plan with the quote: first-article layout on the initial part, in-process checks at each setup, and a final report tied to your datums. If the plan only says “CMM inspected,” ask which features and how often. That is where large-part scrap usually shows up. A shop that answers the red-flag points with specifics is worth more than one that only quotes low.
FAQ
How big can CNC machines go?
Floor-rail gantries exceed 12 m. The real limit is usually crane capacity and door opening, not the machine’s travel.
Can a 4 m part hold under 0.1 mm?
Overall flatness and position typically land in the 0.4–0.8 mm range at that span. Local critical features can be held tighter under temperature control plus laser-tracker assistance.
Plan the print so tight features sit within a 500–1,000 mm zone you can isolate and measure locally, rather than holding the whole envelope tight. Confirm those features one by one, not as a single blanket tolerance.
Is machining or welding cheaper for large parts?
Depends on geometry. Cavity-dominant parts save with fabrication. Rigid low-volume parts are safer as solid machined.
How long does large-part machining take?
Programming and tooling design often eat 30–50% of the lead time. Cutting runs from days to weeks, set by the number of setups and inspection points.
Do I need to provide a CAD model?
For simple parts, a complete 2D drawing is enough. For parts with multiple machined faces, internal cavities, or tight 3D features, send a 3D model (STEP or IGES): it feeds CAM directly and carries the datums. No drawings at all? Our reverse engineering service turns a physical part into a CAD model ready for machining, for legacy components, repairs, or sample replication.