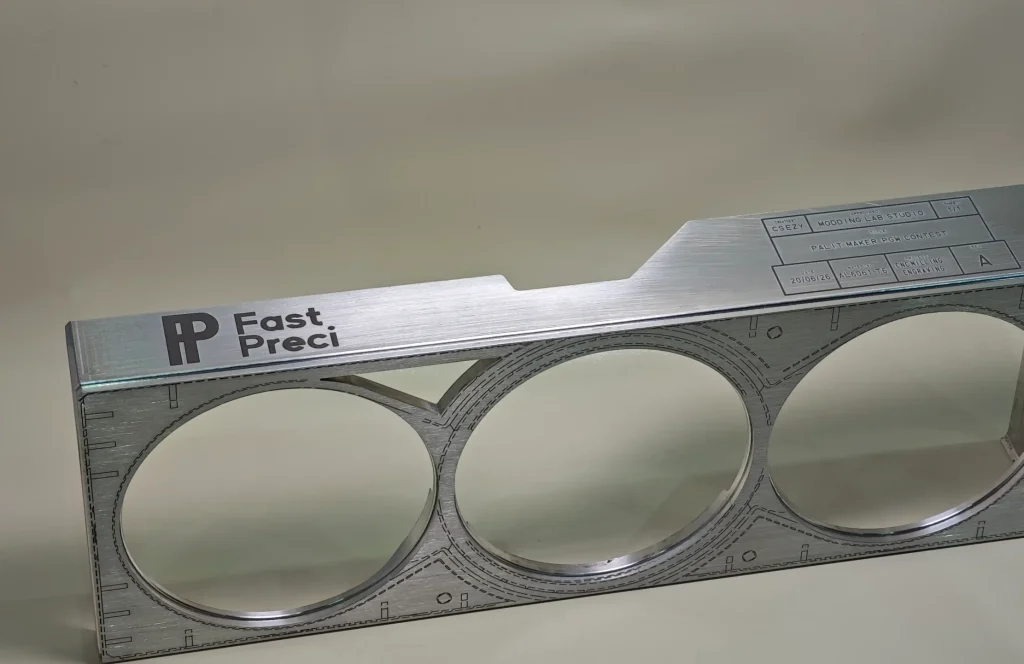
Laser engraving on metal is commonly used to add permanent logos, serial numbers, part numbers, identification codes, and other information to manufactured components. Unlike a printed label or ink marking, laser engraving can create a permanent feature directly on the part surface.
However, the result depends on more than simply selecting “laser engraving” as a process. The metal, surface condition, required depth, final appearance, and manufacturing sequence can all affect the outcome.
For CNC machined parts in particular, these details matter because engraving is often performed on finished surfaces and may need to coexist with tight tolerances, thin walls, anodizing, coating, or other finishing operations.
This guide explains what laser engraving on metal can achieve, which metals are commonly engraved, how depth affects part design, and what information should be specified before production.

Can You Laser Engrave Metal?
Yes. Many common engineering metals can be laser engraved, including aluminum, stainless steel, titanium, brass, and carbon steel.
Laser engraving removes material from the surface to create a recessed feature. Depending on the application, this feature may be a shallow visual mark or a deeper cavity with measurable depth.
Common applications include:
- Company logos
- Part numbers
- Serial numbers
- Data Matrix and other identification codes
- Product information
- Revision markings
- Decorative graphics
- Recesses for paint filling
The final result can vary significantly depending on the metal and its surface condition. A brushed aluminum part, for example, may produce a very different appearance from a polished stainless steel part, even when the same artwork is used.
What Metals Can Be Laser Engraved?
Most commonly used engineering metals can be laser engraved, but the appearance and achievable result vary by material.
Aluminum
Aluminum is widely used for CNC machined housings, enclosures, brackets, heatsinks, and other components. Laser engraving can create recessed text, logos, and identification features on bare, machined, brushed, or anodized aluminum.
Surface condition has a significant effect on the final appearance. Engraving on bare aluminum exposes a recessed surface that may have relatively low visual contrast unless additional finishing, such as paint filling, is used.
Anodized aluminum creates different possibilities. The laser may alter or remove part of the anodized layer, depending on the required result and process. A recessed feature can also be engraved before anodizing if the final finish is intended to cover the engraved surface.
Stainless Steel
Stainless steel is commonly engraved for identification, traceability, equipment markings, and decorative applications. Laser processing can produce visible identification features, while deeper engraving creates a physical recess in the surface.
When engraving stainless steel parts, the required depth, appearance, corrosion considerations, and subsequent finishing operations should all be considered.
Titanium
Titanium components may require permanent identification without adding separate labels or markings. Laser processing can be used for part numbers, logos, and identification information, although the final process should be selected according to the required surface condition and application.
Brass and Other Metals
Brass, carbon steel, and other engineering metals can also be engraved. The final result depends on factors such as surface reflectivity, alloy composition, required depth, and the desired visual contrast.
A clear engraving note should state the intended result, such as surface identification, a specified recess depth, paint fill, or visibility after anodizing, plating, or coating.
How Deep Can Laser Engraving Go?
Laser engraving can range from a shallow surface recess to several tenths of a millimeter or more, depending on the material, feature size, laser process, and part requirements.
For manufactured metal parts, common engraving depths are often between a few hundredths of a millimeter and several tenths of a millimeter. A shallow recess may be sufficient for logos or identification marks, while deeper engraving may be needed for a defined recess, paint filling, or specific durability requirements.
Is a Specific Engraving Depth Necessary?
Not always. If the goal is simply to create a clear logo or part number, specifying the artwork, location, size, and required appearance may be sufficient.
A specific depth is more important when the engraving must:
- Create a measurable recessed feature
- Hold paint or another fill material
- Meet a drawing or technical specification such as AS478
- Maintain a controlled relationship with nearby features
The key question is not how deep the laser can engrave, but how much depth is actually required.
How Depth Affects Cost and Part Design
Deeper engraving generally requires more material removal and processing time, increasing cost—especially for large engraved areas or complex graphics.
Depth should also be checked against the part geometry. For example, a 0.2 mm deep logo may have little effect on a solid aluminum part but could significantly reduce the local wall thickness of a thin-wall housing.
The best approach is to specify the minimum depth needed to achieve the required appearance or function, avoiding unnecessary processing time, cost, and material removal.
How Surface Finish Affects Laser Engraving
The laser interacts with the surface condition of the part, so the same metal can produce different results depending on how it has been machined or finished.
Machined and Bare Surfaces
A machined metal surface may already contain visible tool marks or directional texture. Engraving creates a physical recess, but visual contrast can depend on the texture and reflectivity of the surrounding surface.
Brushed Surfaces
Brushed metal has a directional finish that can affect how logos and text are perceived. A recessed engraving can provide stronger definition, especially when the feature is combined with paint filling.
Anodized Aluminum
Anodized aluminum requires particular attention because the timing of laser processing affects the final result.
Laser processing after anodizing can modify or remove part of the finished surface to create contrast. Engraving before anodizing, on the other hand, allows the recessed feature to receive the final anodized finish along with the rest of the part.
Coated Surfaces
The same principle applies to painted or powder-coated parts. Engraving before coating may leave the recess covered by the final finish, while processing after coating can create contrast by modifying or removing the surface layer.
The desired final appearance should therefore be determined before selecting the manufacturing sequence.

Real Case: Laser Engraving on a Brushed 6061 Aluminum Heatsink Housing
At FastPreci, we CNC machined and brushed a 6061 aluminum heatsink housing, then laser engraved the logo to approximately 0.2 mm and filled the recess with black paint.
Engraving was chosen over surface marking because the design required:
- A recess for black paint fill
- Higher contrast across the brushed texture
- Stronger visual definition for the logo
Before production, we verified that the 0.2 mm engraving depth was compatible with the available wall thickness. The recessed, paint-filled logo provided the required appearance while keeping the engraving depth within the part’s structural limits.
Laser Marking vs Laser Engraving: Similar Process, Different Depths
In manufacturing, laser marking and laser engraving are often used loosely or interchangeably. Both use a laser to add text, logos, serial numbers, QR codes, graphics, or other identification features to a part. In everyday production discussions, both may simply be called laser engraving.
The practical difference is usually the result left on the part—not necessarily the laser machine itself. The same laser system can often create anything from a surface-level contrast mark to a shallow etched detail or a deeper recessed feature by changing the processing parameters, such as power, speed, frequency, focus, fill settings, and number of passes.
Laser marking usually refers to a visible mark at or close to the original part surface. Depending on the material, surface finish, and laser process, the laser may create contrast through discoloration, oxidation, annealing, surface texturing, or very limited material removal. This approach is commonly used when the part needs permanent identification without meaningfully changing its geometry.
Laser engraving usually refers to a deeper result. The laser deliberately removes material to create a recessed feature with measurable depth. This is useful when text, logos, or graphics need to feel sunken, remain visible after paint filling, or meet a specified engraving-depth requirement.
| Required Result | Desired Laser Result | Practical Outcome |
| Serial number, part number, batch code, or traceability code | Surface-level or near-surface mark | Creates permanent identification with little or no measurable effect on part geometry |
| Identification on thin walls, sealing surfaces, or critical functional areas | Surface-level mark with minimal material removal | Helps preserve wall thickness, flatness, and functional performance |
| Recessed logo, text, or graphic | Engraved feature with measurable depth | Material is removed to create a visible sunken feature |
| Logo or lettering to be paint-filled | Engraved recess | The recessed area provides space for paint or other color fill |
| Defined depth on a drawing | Controlled engraved depth | Material removal is controlled to meet the specified depth requirement |
A deeper mark is not automatically the better option. Surface-level marking is often the better choice for permanent identification on precision parts, especially where reducing wall thickness, affecting surface flatness, or changing a critical functional area could create problems.
For quoting and production, focus on the finished result instead of relying only on the terms laser marking or laser engraving. The drawing or RFQ should state whether the feature should remain near the original surface or form a recessed area, together with the marking location, required contrast, approximate or specified depth, paint-fill requirement, surface-finish sequence, and expected service durability.

When Should Engraving Be Done in the Manufacturing Process?
Laser engraving can be performed at different stages of production depending on the required final result.
If a recessed feature should receive anodizing or another surface treatment along with the rest of the part, engraving is typically completed before finishing.
If the objective is to create contrast on an already finished surface, laser processing may be performed after anodizing or coating.
A typical manufacturing sequence might be:
CNC machining → laser engraving → surface finishing
or:
CNC machining → surface finishing → laser processing
Neither sequence is universally correct. The choice depends on questions such as:
- Does the recess need to be anodized or coated?
- Is a contrasting mark required on the finished surface?
- Will the engraved feature later be paint-filled?
- Is the final appearance more important than the physical engraving depth?
Planning the sequence early can prevent unnecessary rework and ensure that the final mark performs as intended.
How to Specify Laser Engraving on Metal Parts
A note such as “laser engrave logo” can leave too much open to interpretation. For a predictable result, define the content and location, the required appearance, and any finishing constraints.
Include the text, logo, code, or artwork; its position, orientation, and size; and an approved vector file where needed. State whether the feature should be surface-level or recessed, along with any depth, contrast, paint-fill, or durability requirement.
Also note the local surface condition and whether engraving should be completed before or after anodizing, plating, coating, or other finishing. These details can affect the final appearance and readability of the mark.
A simple serial number may need only the content and location. A visible logo on a finished precision part usually requires more detailed specifications.
Frequently Asked Questions
Does laser marking remove material?
Laser marking changes the surface rather than cutting a cavity into it. The beam may oxidize, anneal, or restructure a thin surface layer. Some marking processes remove a small amount of material, but removal stays minimal compared with engraving. Laser engraving removes material by vaporization and leaves a recess that can be measured.
Will laser marks survive anodizing or powder coating?
A mark applied before these finishes is generally covered by the coating. When the laser should modify or remove the finished layer, the marking step runs after the treatment, as with white marks on anodized aluminum. When a recess should receive the finish along with the rest of the part, engraving runs before it. The sequence follows the required final surface.
Can Laser Engraving Create Black or White Marks?
Yes. Laser engraving can create black, white, or other high-contrast effects, depending on the material, surface finish, laser process, and processing parameters.
On light-colored or machined metal surfaces, laser processing can often produce dark or black marks. On darker surfaces, it may create light or white marks when the laser produces sufficient contrast. When a specific color is required, the engraved recess can also be paint-filled after processing.
Does laser engraving weaken aluminum parts?
The effect depends on the engraving depth, wall thickness, feature geometry, and alloy. A shallow recess in a part with adequate wall thickness has little practical effect. A deeper recess in a thin wall reduces the load-bearing section and can act as a stress concentration. Engraved depth is checked against wall thickness and dimensional requirements before release.
Need Help Defining the Right Laser Mark?
Not sure whether your part needs a surface mark, shallow engraving, or a deeper recessed feature? Send us your drawing or CAD file along with the marking location, artwork, material, surface finish, and desired result.
Our engineering team can help review the design, identify potential issues with thin walls, critical surfaces, or downstream finishing, and recommend a practical marking or engraving approach before production starts.