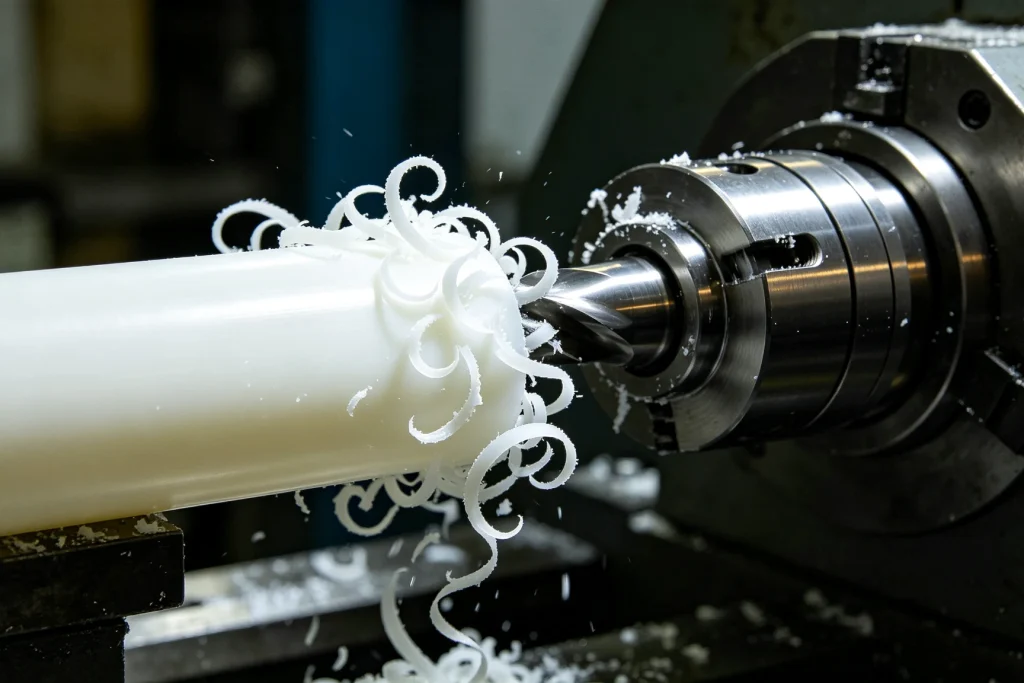
You have a drawing that calls out PTFE (often called Teflon) for a valve seat, seal, or insulator. The material selection is usually sound. PTFE machining is fast; sharp carbide tooling cuts the stock cleanly and freely. The problem is accuracy, not cutting: the part deforms under clamping force and changes size with temperature, so holding it to print is where most of the risk sits.
Clamping is the limiting step more often than any other. Forces that Delrin or nylon absorb without measurable distortion mark PTFE and shift the feature you are trying to hold. Thermal expansion is the second source of trouble: PTFE’s coefficient runs roughly ten times that of carbon steel, so a dimension checked while the part is still warm from the cut can drift out of tolerance before it reaches incoming inspection. Both are material behavior rather than process defects, and both surface after machining.
This guide covers the decisions to make before you release the drawing for quotes: the tolerance range that belongs on a PTFE print, clamping and deburring methods that keep soft features intact, why dimensions keep moving after machining, and when a filled grade, or a switch to PEEK or Ultem, is the better fix than tightening process control. On a PTFE CNC machining order, workholding and inspection decide success more than cutting does.
Machined PTFE parts concentrate in a few families: valve seats, seals and bushings, electrical insulators, and wetted components for chemical, semiconductor, and food-handling equipment. If your part falls into one of these, the sections below are the checks to run before the file goes out.
Why Is PTFE Difficult to Machine?
PTFE is difficult to machine because it is soft, slick, and dimensionally unstable under heat and load. The cutting itself is straightforward; the challenge is that each property affects what happens around the cut: how the part is held, how edges come off the tool, and how dimensions behave afterwards.
Low Stiffness and Tool Deflection
PTFE is among the softest machined plastics, with stiffness far below PEEK or nylon. Cutting force bends the material ahead of the tool instead of lifting a clean chip, so thin walls and seal lips deflect rather than hold shape. Features routine in metal need wider tolerances or extra support during machining.
Slickness vs. Clamping Force
Low friction is what makes PTFE work as a seal or bearing surface, but at the vise it works against you: the part wants to slide out of the jaws. More clamping force fixes that, and more clamping force deforms a soft material. A PTFE blank clamped like a steel block ends up with jaw marks and a distorted feature; clamped gently, it slips out of position.
Thermal Expansion and Creep
PTFE’s coefficient of thermal expansion runs roughly 100–150 × 10⁻⁶/°C, which is why a part checked while still warm from cutting can be out of tolerance once it cools. Under sustained load the material also creeps, so a dimension that passes today may not hold in service. Tolerances and inspection timing both have to account for this.
None of this makes PTFE impractical to machine. It means the process plan, not the cutting, is where an order succeeds or fails: clamping, deburring, print tolerances, and inspection timing all need to be set for this material.

Why Do PTFE Parts Change Size After Machining?
PTFE parts change size after machining for three reasons: cooling, stress release, and creep. They act on different timescales, so size can keep changing after the part leaves the machine.
Machining heats the material locally. A dimension checked while the part is still warm reflects the expanded part, not the room-temperature one; once it cools, the same dimension can sit outside tolerance. Thin walls and long features move most.
PTFE stock carries residual stress from molding or extrusion. Removing material lets that stress redistribute, and the part relaxes into a slightly different shape, often hours or days after the cut. The effect is strongest when a large or asymmetric amount of material is removed.
Creep is the slow part. Under sustained compression, as in a seal or gasket, the material keeps deforming over weeks or months and loses original height. That is not a machining error; it is the property that lets PTFE conform and seal.
Two checks keep this under control. Machinists commonly let PTFE parts sit before final measurement and recheck critical dimensions. On the drawing, separate critical assembly dimensions from free ones, and specify that they are measured after the part stabilizes.
How Do You Clamp PTFE Parts Without Crushing It?
The rule for clamping PTFE is to spread the load over as much area as possible and avoid point contact. Three methods cover most parts: padded jaws, counterbored hold-down holes, and vacuum.
Padded jaws are the simplest fix. Soft padding between the jaws and the part spreads the force, so a steel vise no longer leaves marks in PTFE. They suit blocky parts and light cuts; on heavy cuts the part can still shift, because the padding reduces grip.
Counterbored hold-down holes are the most reliable option. The drawing adds clearance holes with a flat counterbore, and the part screws to a fixture plate instead of being squeezed from the sides. This is often worth specifying at the design stage: two non-functional holes remove the clamping risk entirely.
Vacuum chucks suit thin, flat parts where any jaw force would bow the material. The load is uniform, so thin sheets hold their shape. They fail on parts with through-holes, which break the vacuum.
Choose by part geometry: padded jaws for simple blocks, hold-down holes for accuracy-critical or thin work, vacuum for flat sheets. If the part is thin and tolerances are tight, hold-down holes are the safer default than soft jaws.
How Do You Deburr PTFE Parts Without Damaging It?
The best way to deburr PTFE is to make fewer burrs in the first place. Burrs on soft plastics come from the cutting step: a dull edge tears the material loose instead of shearing it, and a ragged edge is harder to clean up. Sharp tooling is the first defense.
Dull tools are the main burr source. A worn edge bends and tears the soft material, leaving a ragged edge that resists removal. Sharp carbide and moderate speeds shear the surface, so edges come off clean. Fewer burrs at the tool means less work at the bench.
What remains comes off by hand with a light touch. A sharp knife skims the edge; pressure digs into the soft surface and leaves a visible scratch or gouge. One heavy pass can ruin a sealing surface. Work in short strokes and check the edge by feel.
Designing chamfers or edge breaks into the part can eliminate secondary deburring. When specified on the drawing, the feature is machined directly in the toolpath, removing burrs with the cutting chip rather than by hand.
This avoids manual finishing on soft or critical sealing surfaces and adds minimal cycle time. Specify chamfers or edge breaks on parts that will be handled or assembled; keep edges sharp only when required for function.
PTFE Machining Tolerances: What to Realistically Expect
PTFE machining holds wider tolerances than metal, and the print should reflect that. Standard machining holds roughly ±0.1 mm on most features; ±0.025 mm is achievable on selected dimensions, but only with extra process care and cost. Metal-level tolerances are not realistic in PTFE.
Realistic Tolerance Bands
| Tolerance band | Typical range | Where it applies | What it requires |
| Standard | ±0.1 mm | free dimensions, non-sealing features | normal cycle time and inspection |
| Precision | ±0.025 mm | critical assembly and sealing features | stabilization, extra inspection, higher scrap risk |
These figures are commonly quoted industry ranges, not a guarantee for every geometry. Thin walls, long features, and blanks carrying high residual stress sit at the wide end of the band; a short, thick part can hold tighter. Confirm the band with the machinist before the print is released.
Why PTFE Tolerances Run Wide
The reasons are the material properties covered earlier. Cutting force deforms the soft part while it is held, temperature moves dimensions after the cut, and creep shifts them under sustained load. Each one adds dimensional uncertainty that a metal print does not have, so PTFE tolerance bands sit wider than steel or aluminum for most geometries.
Where Tight Tolerances Belong on the Print
Assign tight tolerances only to features that mate with other parts or carry a sealing function, and let the rest run at the standard band. A print that calls ±0.025 mm everywhere raises cost through extra inspection and scrap, and it gives the shop less room to protect the dimensions that matter. Most PTFE parts machine successfully on the standard band; reserve precision for the two or three features that genuinely need it. For how these bands hold up across part geometries, the plastic machining service page covers the process in more detail.
Virgin vs Filled PTFE: Which Grade to Specify
Specify virgin PTFE for seals, gaskets, and electrical insulators; move to a filled grade only when the part carries load, resists wear, or sheds heat.
What Each Filler Adds and Costs
| Grade | What it adds | What it costs |
| Virgin | chemical inertness, electrical insulation, low friction | soft, creeps, wears faster under load |
| Glass-filled | stiffness, wear resistance, lower creep | higher friction, wears mating surfaces |
| Carbon-filled | stiffness, thermal conductivity, lower creep | becomes electrically conductive |
| Bronze-filled | load capacity, wear resistance, heat conduction | heavy, conductive, abrasive to mating parts |
| Graphite-filled | self-lubrication, thermal conductivity | slightly lower strength |
Filled grades raise friction but cut wear. Only glass-filled PTFE stays insulating; carbon, bronze, and graphite conduct.
Why Virgin PTFE Remains the Default
Seals and gaskets work on surface properties: low friction, inertness, conformability. For many sealing applications, creep is managed primarily through part and seal design rather than by adding fillers.
When Filled Grades Earn Their Trade-offs
Bearings and wear rings run on bronze- or carbon-filled PTFE, typically improving wear life several times over virgin. Structural parts take glass or carbon for creep resistance; hot-running parts take carbon or graphite for conductivity. Confirm grade availability with the supplier before quoting.
PTFE vs PEEK vs Ultem: When to Switch
PTFE stays the right choice for most seals, gaskets, and insulators. Switch to PEEK or Ultem only when the service condition exceeds PTFE’s limits: continuous heat, sustained load, or a sealing feature that must hold shape under pressure.
How the Three Materials Compare
The table compares the three:
| Property | PTFE | PEEK | Ultem |
| Continuous temperature limit | ~260 °C | ~250 °C | ~170 °C |
| Mechanical strength | low, flexible | high, rigid | high, rigid |
| Creep under sustained load | high | low | low |
| Sealing friction | low | higher | higher |
| Relative cost | $ | $$$ | $$ |
| Machinability | soft, easy to distort | rigid, stable cuts | rigid, stable cuts |
Temperature figures are typical published limits, not guarantees.
When Seal Geometry Requires a More Rigid Material
The switch usually happens at one sealing feature, not across the whole part. A PTFE seal lip creeps under sustained load: contact pressure drops, the lip relaxes, and the joint starts to leak. PEEK or Ultem hold the lip geometry, so the seal keeps its sealing force over time. High temperature can drive the switch, but sustained load and dimensional stability are often equally important.
Where Each Material Wins
Keep PTFE where conformability and low friction do the job: gland seals, chemical and food-grade liners, and electrical insulators. Move to PEEK for valve seats, pump components, and semiconductor parts that hold tolerances and resist wear; it machines cleanly and keeps shape, as covered in our PEEK machining guide. Ultem suits the same rigid geometry at a lower cost, with a lower temperature ceiling. Confirm both grades with the supplier before quoting; stock varies by shop.
Key Decisions Before You Send the Drawing
PTFE is easy to cut but difficult to hold dimensionally. Keep tight tolerances only on functional features, minimize clamping force, and inspect critical dimensions after the part stabilizes. Choose filled PTFE, PEEK, or Ultem only when load, wear, temperature, or dimensional stability exceeds what virgin PTFE can reliably handle.
Send us your drawing for a quote. Our engineers can review tolerances, workholding risks, and material selection before production.
Frequently Asked Questions
What are the most important tips for machining PTFE?
Use sharp tools, light cutting forces, and gentle clamping. Padded jaws or counterbored hold-down holes stop the part from distorting under cutting force. Sharp edges cut cleanly; dull ones tear the surface.
Can PTFE be threaded or tapped effectively?
Yes. Coarser threads generally perform better than very fine threads in soft PTFE. For small threads or joints subject to repeated or high loads, metal inserts can provide better durability.
Is PTFE safe to machine?
Yes, under normal machining conditions. PTFE should not be overheated, because thermal decomposition at elevated temperatures can produce hazardous fumes. Use sharp tools, control heat buildup, and provide appropriate ventilation.
Is PTFE the same as the non-stick coating on cookware?
The material is the same PTFE. Cookware uses it as a thin sintered coating on metal. Machined parts come from solid bar or sheet stock, which cuts differently under the tool.
Can PTFE be bonded or glued?
Not with ordinary adhesives. PTFE’s surface energy is roughly 18–20 mN/m, so most glues cannot wet it. Use sodium-etch pretreatment or design a mechanical interlock into the part.
When should PFA or PCTFE be used instead of PTFE?
PFA where weldability or clarity matters; PCTFE where moisture permeation must be minimal. Both trade off: PFA costs more; PCTFE loses some strength.