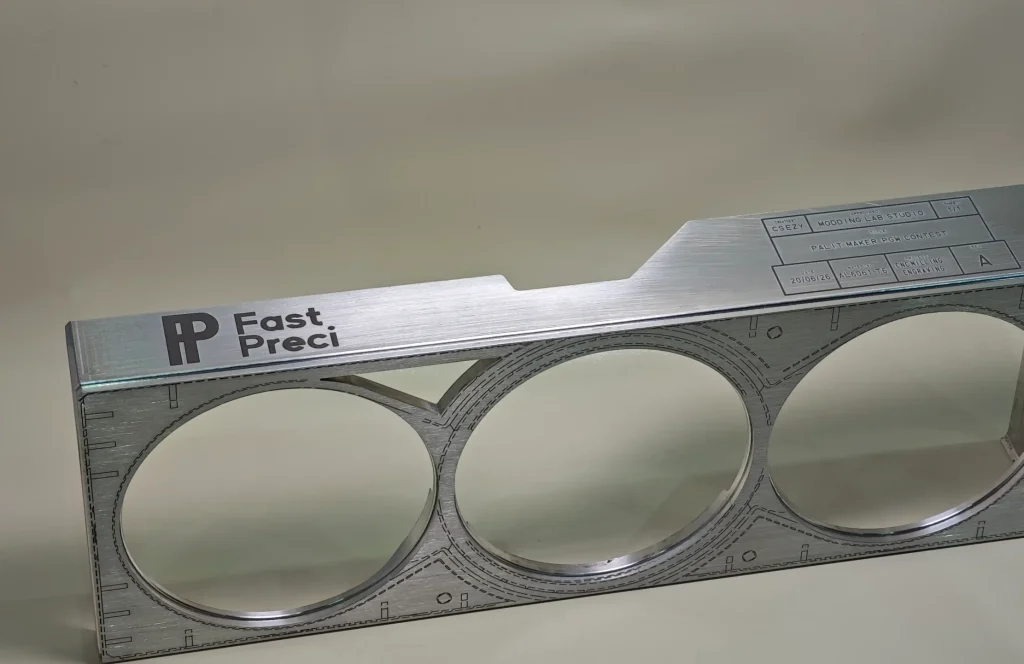
Semiconductor machining produces custom mechanical parts used around semiconductor manufacturing and inspection operations. It covers the structures, fixtures, fluid-handling hardware, motion components, and support parts that enable the process equipment.
An acceptable part is not defined by one dimension alone. The drawing may combine positional tolerance, surface condition, burr control, material traceability, cleaning requirements, and repeatability. This article helps engineers and buyers decide what belongs on the drawing, what to resolve during DFM, and what to verify before release.
For an overview of available processes and request support for a specific project, see our semiconductor machining services.
What Is Semiconductor Machining?
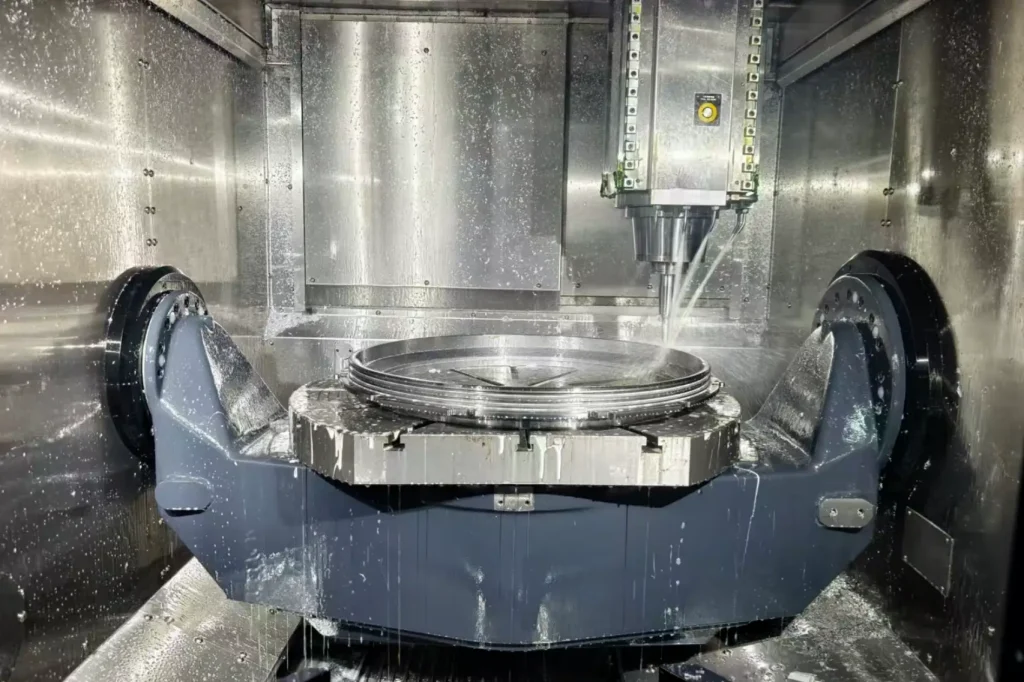
CNC machining supports the equipment surrounding chip production rather than the wafer fabrication process itself. Typical machined components include vacuum hardware, gas manifolds, wafer-handling components, alignment fixtures, inspection tooling, structural frames, and electrical insulation parts.
These components require stable dimensional control, material compatibility, and reliable performance in precision equipment environments. FastPreci provides CNC machining support for semiconductor-related applications, manufacturing metal and engineering plastic components used in equipment alignment, inspection, and other critical support functions.
What Makes Semiconductor Machining Demanding
The difficult part is usually the combination of requirements. A component can meet its dimensional drawing and still fail the application if a burr breaks loose, a blind feature retains contamination, a sealing face distorts, or the material documentation is incomplete.
Start from function, not the tightest tolerance on the drawing.
Flatness and surface condition can matter more than a general linear tolerance on a cover, interface, or locating surface. The machining route must then control residual stress, fixturing load, and material removal sequence rather than simply adding a tighter inspection limit.
Consider thermal and material behavior early.
Aluminum can move with temperature, and thin sections can shift after material removal. Rough machining, stabilization or stress relief where required, and final machining of critical features may be necessary.
Plan cleanliness during machining.
Blind holes, sharp internal corners, inaccessible channels, and aggressive toolpaths can create later cleaning problems. Flag them in DFM; cleaning cannot always remove trapped residue or an attached burr.
In semiconductor applications, particle and contamination control can be a functional requirement rather than a cosmetic preference. Relevant equipment and process expectations are addressed through SEMI standards for semiconductor equipment.
Validate a process, not just one sample.
A first article is a starting point. Production confidence comes from controlled datums, fixtures, inspection, material lots, and revisions.

Common Components in Semiconductor Applications
The following categories help determine which engineering questions should be raised before manufacture:
| Application area | Typical machined parts | Questions that drive the process |
| Fluid and gas delivery | Manifolds, valve bodies, fittings, distribution plates | Are internal passages cleanable and inspectable? Which media contact the material? |
| Vacuum and process interfaces | Flanges, chamber hardware, sealing covers, mounts | Which faces seal or locate? Are flatness, finish, cleaning, or leak-test requirements specified? |
| Wafer handling and motion | End-effectors, guide elements, robot interfaces, carriers | What may contact the wafer? Which surfaces control motion, mass, wear, or particle risk? |
| Mask, alignment, and inspection | Mask holders, alignment tools, inspection fixtures, reference blocks | What are the functional datums? Which hole patterns and contact faces must remain stable? |
| Support and service tooling | Centering tools, insulating parts, templates, jigs | What must be repeatable during setup, maintenance, or inspection? |
This classification guides the drawing review: define functional interfaces, identify contamination-sensitive surfaces, and separate critical features from dimensions that can use a broader manufacturing allowance.
Materials for Semiconductor Components
Material selection should be tied to the application environment, not treated as a generic semiconductor-materials checklist.
Aluminum alloys suit many structural parts, holders, frames, and interfaces where low mass, machinability, and thermal conductivity matter. Fix the alloy and temper on the drawing when stability or finishing response matters. Specify the function of any finish, not only its name.
Stainless steels, including 304 and 316L, are considered where corrosion resistance, stiffness, or compatibility with process media is needed. Specify material certification, surface condition, and any additional cleaning when relevant.
Engineering plastics are useful for insulating parts, fixtures, guides, and non-metal contact features. PEEK, PTFE, Delrin, and PVC are not interchangeable. PEEK is used where temperature and chemical resistance justify its cost; Delrin is practical for stable, low-friction fixtures; PTFE meets specific chemical-resistance needs but has different stiffness and creep behavior. Do not copy a metal tolerance onto a plastic feature without reviewing moisture, thermal exposure, and contact load.
Ceramics and composites can suit insulation, stiffness, heat resistance, or low thermal expansion requirements. Review their geometry and finishing constraints before release.
Material documentation is part of the selection decision. If the application needs a particular alloy, resin grade, temper, lot traceability, or certificate, identify it in the purchase package. A material name alone may not define the form, grade, or documentation required for a critical component.
For broader material-process options, see metal CNC machining and plastic CNC machining.

Selecting Processes and Surface Treatments
Choose the process from the feature, not from an equipment list. Multi-axis milling helps hold several faces or angled relationships in one setup; turning suits rotational features; grinding addresses selected flatness, roundness, or surface requirements; and wire EDM can help with narrow features in conductive materials. Minimize unnecessary setups while preserving an inspectable datum strategy.
Surface treatment also needs a stated purpose. Anodizing may provide electrical insulation, corrosion resistance, or wear behavior on aluminum. Stainless steel may need specified cleaning, passivation, or electropolishing. The drawing should identify critical surfaces, masking, inspection method, and acceptance criteria. Available routes are listed in our surface finishing services.
Manufacturing Challenges to Resolve Early
Burrs and particle traps.
Burrs can affect fit, move during use, or make a feature difficult to clean. Define critical edges around holes, slots, channels, and contact surfaces. Avoid inaccessible sharp corners without a functional purpose.
Thin-wall distortion.
Thin sections can move during clamping and after material removal. A revised wall layout, staged machining, controlled stock removal, or a different datum and fixture plan may be more effective than a tighter tolerance.
Sealing and locating faces.
A face can be dimensionally correct but fail to seal or locate if its flatness, surface condition, or datum relationship is unclear. Call out the functional requirement and inspection method.
Residue and revision control.
Define cleaning, drying, packaging, labeling, and documents in the quote package. Use revision-controlled 2D and 3D files, and ensure inspection records reference the controlling revision.
Inspection access.
A critical feature must be measurable after machining and finishing. During DFM, confirm the datum scheme, probe access, gauge access, and whether the stated result will be reported by CMM, surface measurement, a functional check, or another agreed method. An unmeasurable requirement creates avoidable disagreement after production.
How to Choose a Semiconductor Machining Supplier
A supplier review should test how the shop handles uncertainty, not only what machines it owns.
- Ask for DFM feedback before release. It should identify datum, thin-wall, internal-corner, finish-allowance, tolerance, and inspection-access risks.
- Match evidence to the part. Confirm the first-article report, CMM data, surface measurement, material certification, and lot traceability actually needed for critical features.
- Clarify cleaning and packaging. Controlled cleaning, protective packaging, labeling, and documentation affect routing and cost.
- Review repeat-order control. Ask how fixtures, programs, inspection points, and approved samples are retained or documented.
- Evaluate a real drawing. The quote stage shows whether the engineering team asks questions that prevent rework.
At FastPreci, every project starts with a DFM review to identify potential manufacturing risks before quotation. Submit your drawing and requirements for engineering review.
FAQ
What tolerance is typical for semiconductor machined parts?
There is no single semiconductor tolerance. A critical sealing face, an alignment pattern, and a service fixture can have very different requirements. Define tolerance, flatness, surface condition, and inspection method from the feature’s function rather than applying the same value across the drawing.
Do all semiconductor-related parts require cleanroom manufacturing?
No. Requirements depend on where the part is used and what it contacts. Some parts require controlled cleaning and packaging, while fixtures or external support parts may have different requirements. State the intended environment and cleanliness expectation during quoting.
Can CNC machining support both prototypes and repeat orders?
Yes. CNC machining is suitable for prototype iterations because it does not require dedicated production tooling. For repeat orders, the manufacturing plan should preserve the approved material, fixture approach, program revision, inspection points, and documentation requirements.
What information should be included in a semiconductor machining RFQ?
Provide the 2D drawing, 3D model, material specification, quantity, surface finish, critical tolerances, and inspection requirements. For semiconductor equipment parts, details such as vacuum compatibility, cleanliness needs, and functional interfaces are also important. FastPreci can help review drawings and clarify manufacturing requirements before quotation.