Project Overview
Hyoku Team, a STEM racing team based in Brazil, needed 12 prototype rear wheels for a miniature racing car. The project involved precision PEEK CNC machining for wheels with a 0.5 mm outer rim and a tight concentricity requirement of ±0.03 mm.
The customer had previously experienced deformation and uneven rotation with wheels from another supplier. For this thin-walled PEEK component, the central manufacturing challenge was maintaining the required concentric relationship between the hub and outer rim without allowing clamping forces or machining forces to distort the geometry.
| Project Detail | Specification |
| Customer | Hyoku Team, Brazil |
| Application | STEM Racing miniature rear wheel |
| Material | PEEK |
| Quantity | 12 prototypes |
| Outer Diameter | Ø28.2 (+0.2/0) mm |
| Overall Width | 15.2 (+0.2/0) mm |
| Outer Rim Thickness | 0.5 mm |
| Concentricity | ±0.03 mm |
| Surface Roughness | Ra 3.2 |
| Turnaround | 7 calendar days |
The Challenge: Keeping a Thin PEEK Rim Concentric
The main challenge was not simply machining PEEK. It was finishing a very thin outer rim without allowing it to deform or lose alignment with the central hub.
The wheel combines a 0.5 mm outer wall with a lightweight internal structure of six spokes and a thin central web. With such limited structural rigidity, the outer rim is sensitive to machining forces and support conditions.
For this project, we paid particular attention to three things: where to establish the central reference, how to fixture the part without introducing distortion, and how to support the thin rim during final machining.

Our Approach: Establish the Center First, Then Support the Rim
We arranged the machining sequence and workholding approach around the most deformation-sensitive features, using controlled clamping and support locations to avoid distortion during machining:
Rough machining → Internal feature finishing → Plaster backfilling → Outer profile finishing → Plaster removal
The principle was straightforward: finish the critical internal geometry first, then provide temporary support before bringing the thin outer rim to its final dimensions.
1. Rough Machining
We first removed the bulk of the material while the workpiece remained rigid, completing roughing before bringing the thin-wall features to their final dimensions.
2. Finish the Internal Features First
We finished the central hub and internal structure first, establishing the central geometry as the reference for the outer rim. This machining sequence helped maintain the required concentricity while minimizing deformation of the thin wall.
3. Add Temporary Plaster Support
After the internal features were completed, we filled the cavity with plaster. Once cured, the plaster provided temporary backing behind the thin outer rim, adding rigidity during the final machining operation. Together with controlled workholding, this helped reduce the risk of distortion caused by both clamping and cutting forces.
4. Finish the Outer Rim
With the internal support in place, we finished the outer perimeter to the required Ø28.2 mm diameter and 15.2 mm overall width. The temporary support helped reduce unsupported movement of the thin PEEK wall and allowed the outer profile to be finished relative to the previously established central hub. After machining, the plaster was removed and washed out from the internal cavity.

Inspection: Verifying Concentricity with CMM
The critical inspection focus was the central bore, outer geometry, and their concentric relationship.
The Ø6.5 mm central bore and outer geometry were inspected using a CMM (Coordinate Measuring Machine). The CMM was used to measure the relevant features and verify the required ±0.03 mm concentricity between the central hub and outer rim.
Because the outer rim was only 0.5 mm thick, the inspection setup and measurement approach were carefully controlled to minimize the risk of deforming the part during measurement.
Result
All prototype PEEK wheels were completed and delivered to Brazil within the required turnaround.
After receiving the parts, Hyoku Team shared the following initial feedback:
“Hi Cori! Hope this message finds you well. Just to tell you that we’ve just received the parts and everything it’s ok. Thank you for everything Now we going to look the quality of the wheels, but it seems perfect me”
What This Project Taught Us About PEEK CNC Machining
For thin-walled PEEK components, we found that the key is not simply choosing the right machining process. How the part is supported and when each feature is finished can have a major impact on the final geometry.
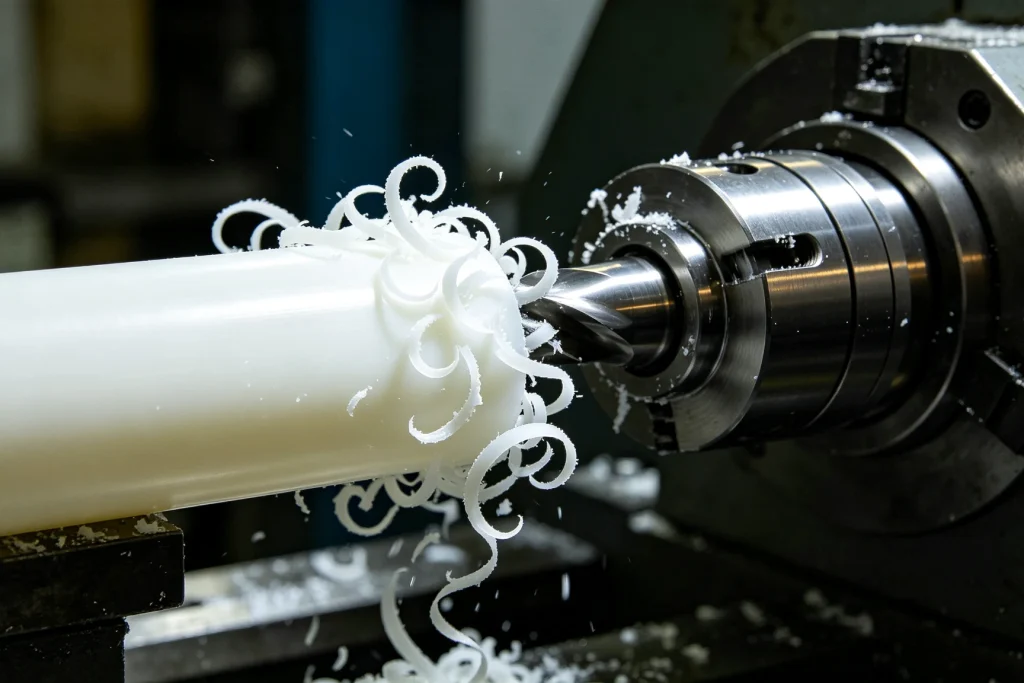
These considerations also apply to many other precision plastic components—not only PEEK wheels. Different engineering plastics respond differently to cutting heat, clamping force, internal stress, and thin-wall machining conditions. Learn more about our plastic CNC machining services, including material options, prototype support, and precision machining approaches for custom plastic parts.
Three considerations from this project are particularly relevant:
- Establish critical central features first. Finish the hub and other reference features before bringing the most flexible outer features to final size.
- Support thin polymer walls during final machining. Temporary internal support can reduce unsupported deformation when machining very thin PEEK structures.
- Match inspection to part rigidity. For flexible features, non-contact measurement can help avoid measurement errors caused by physically deflecting the part.

Need to Machine a Thin-Walled PEEK Part?
Thin-walled PEEK components can require more than simply selecting the right cutting parameters. Part support, machining sequence, and inspection method can all affect the final geometry.
If your PEEK part has thin walls, tight concentricity requirements, or other deformation-sensitive features, send us your drawings and requirements. Our engineers can review the geometry and recommend a suitable CNC machining approach.
Frequently Asked Questions
1. Can FastPreci CNC machine thin-walled PEEK parts?
Yes. Thin-walled PEEK parts can be CNC machined, but the machining strategy needs to account for the material’s relatively low rigidity and the risk of deformation. For this wheel, we used a staged machining sequence and temporary internal support to control the thin outer rim.
2. How do you prevent deformation when CNC machining thin-walled PEEK?
The approach depends on the part geometry. For this project, we finished the internal features first and then used temporary plaster support before machining the thin outer rim. This provided additional backing to the 0.5 mm wall during the final operation.
3. Can CNC machining achieve tight concentricity on PEEK parts?
It can, provided that the part is properly supported and the machining sequence is planned around the critical reference features. In this project, the required concentricity between the central hub and outer rim was ±0.03 mm.
4. Why was plaster used when machining this PEEK wheel?
The plaster was used as temporary internal support. The thin outer rim had limited structural rigidity, so filling the internal cavity provided backing during the final outer-profile machining operation. The support was removed after machining.
5. What should I consider when designing a thin-walled PEEK part for CNC machining?
Wall thickness, feature geometry, workholding, machining sequence, and critical tolerances should all be considered together. If a very thin wall must maintain a tight relationship with another feature, it is worth discussing the manufacturing approach before finalizing the design.